Selecting Glassfiber Reinforced Epoxy Pipe for Pressure and Temperature Duty
Selecting Glassfiber Reinforced Epoxy Pipe for Pressure and Temperature Duty
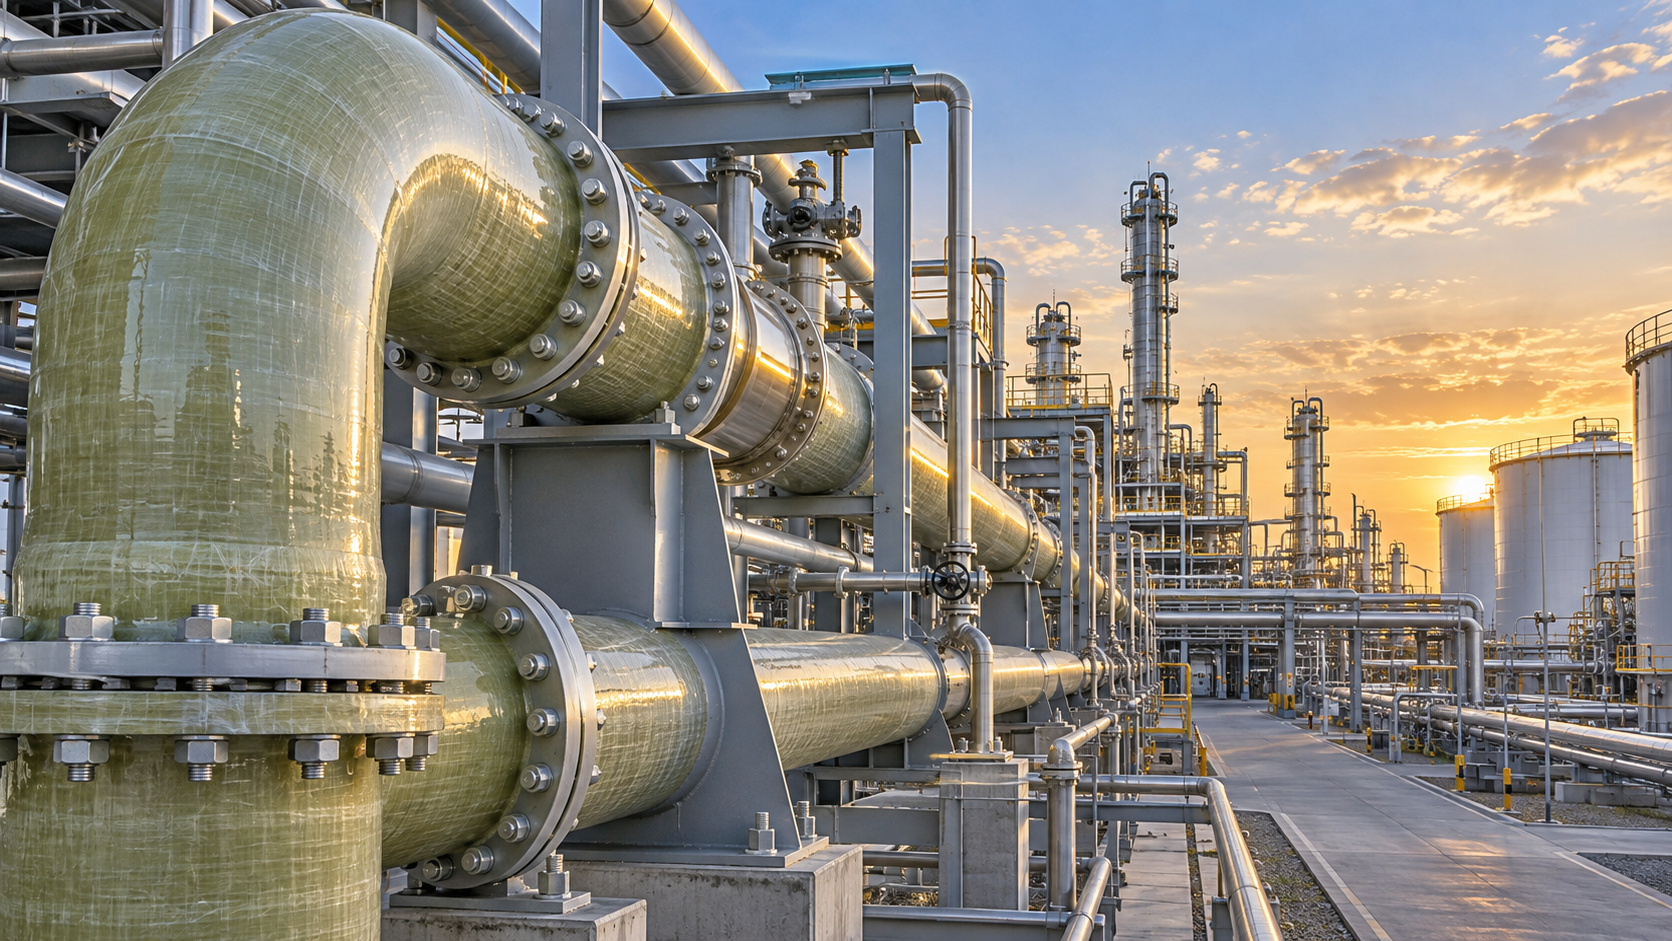
Selecting a Glassfiber Reinforced Epoxy Pipe for oil, gas, marine, refinery, and chemical service is not a matter of matching a nominal diameter to a line list. The difficult part is establishing whether the complete pipe system—pipe wall, resin system, fittings, joints, supports, and installation method—can remain reliable through its actual pressure and temperature history.
That distinction matters because GRE piping usually performs very well in corrosive fluid service, but it does not respond to pressure, heat, cyclic loading, or poor installation in exactly the same way as steel. A technically sound evaluation therefore starts with the operating envelope, not with a catalog pressure class. For a process line that sees only stable ambient-temperature water, the decision path may be relatively straightforward. For produced water, seawater injection, refinery drains, hot chemical transfer, LNG-related utility systems, or ballast piping, the assessment becomes more demanding.
The practical question is not simply, “Can GRE replace metal here?” It is: “Under the most severe credible combination of pressure, temperature, fluid chemistry, and mechanical loading, will this specific GRE system remain within its qualified design limits?”
Start With the Real Operating Envelope
A pipe specification should distinguish normal operation from upset, start-up, shutdown, cleaning, hydrotest, and emergency conditions. In many projects, the normal pressure and temperature are easy to obtain from the process team. The overlooked conditions are often more decisive: a short high-temperature cleaning cycle, a pump dead-head event, a blocked outlet, pressure pulsation, vacuum during drainage, or a high test pressure applied before the line is fully restrained.
For Glassfiber Reinforced Epoxy Pipe, pressure and temperature cannot be assessed independently. As service temperature rises, the allowable pressure capability of a composite piping system may need derating in accordance with the manufacturer’s qualified data and applicable project standard. The resin matrix is particularly relevant here. Fibers carry much of the tensile load, but resin selection influences chemical resistance, thermal behavior, interlaminar performance, and long-term durability.
A good inquiry package should therefore state the maximum continuous operating temperature, expected peak temperature, design pressure, surge pressure, design life, fluid composition, and the frequency of thermal or pressure cycling. “Water service” is not enough. Salinity, dissolved oxygen, hydrocarbons, solids, chlorides, treatment chemicals, pH range, and cleaning media can all change the material decision.
Where process information is still developing, it is better to identify assumptions openly than to select an aggressive pressure-temperature rating based on incomplete data. A conservative assumption can later be refined; an undocumented assumption can become a field failure argument.
Pressure Rating Is a System Question
Technical evaluators sometimes focus on the straight pipe pressure rating and treat fittings as a secondary procurement item. That is risky. In a GRE system, elbows, tees, reducers, flanges, adhesive-bonded joints, laminated joints, and transitions to steel must all be evaluated for the same duty. A nominally high-rated straight pipe does not compensate for a weak point at a branch connection or a poorly detailed flange transition.
The winding design is central to this evaluation. Hoop-oriented reinforcement supports internal pressure resistance, while axial reinforcement contributes to longitudinal loads and system stability. The exact laminate design should be appropriate to the project’s pressure duty, joint arrangement, and mechanical requirements. It is not enough to compare wall thickness between suppliers; two pipes with similar thickness may have different fiber architecture, resin content, stiffness, and qualification basis.
Surge deserves separate attention. Pump starts and stops, fast-acting valves, compressor-related transients, and abrupt changes in flow direction can create pressure events well above steady-state conditions. The piping designer should establish the expected transient load rather than assume that the normal operating pressure contains sufficient margin. This is especially important on long water injection and seawater systems, where hydraulic transients can govern parts of the design.
External pressure also needs a deliberate check. GRE lines can be vulnerable to collapse or ovalization when subject to vacuum, buried installation loads, submerged duty, or negative pressure caused by rapid draining. A line that is safe under internal pressure is not automatically adequate for vacuum duty. If vacuum is credible, it should be specified at the beginning, together with any need for stiffening, burial design verification, or vacuum breakers.
Temperature Duty Is About More Than Heat Resistance
High-temperature selection is often reduced to a single maximum temperature figure. In practice, temperature cycling can be just as important as the peak value. A line that repeatedly moves from ambient conditions to elevated temperature will expand, contract, and transfer loads to guides, anchors, joints, equipment nozzles, and steel transition pieces. GRE has a different thermal expansion behavior from carbon steel, so mixed-material systems need particular care.
A refinery utility line may have a short section of GRE connected to a steel pump spool, steel tank nozzle, or metallic valve assembly. If the pipe is tightly restrained without a proper flexibility review, thermal movement can be forced into joints or flange faces. The visible symptom may be leakage at a connection, but the underlying issue is often support design rather than the pipe itself.
Temperature also affects the chemical environment. Some media that are acceptable at ambient conditions can become more aggressive at elevated temperature. The evaluation should therefore use the actual fluid concentration and highest credible operating temperature, not separate chemical and thermal statements taken from different documents.
Resin Compatibility Must Be Verified for the Actual Fluid
“Epoxy” is not a complete chemical-resistance answer. Glassfiber Reinforced Epoxy Pipe may use resin systems formulated for different combinations of temperature, chemicals, hydrocarbon exposure, and water service. The correct choice depends on the full medium, including additives that may only be present during cleaning, commissioning, or intermittent treatment.
For example, a produced-water line can include salts, residual hydrocarbons, scale inhibitor, biocide, oxygen scavenger, suspended solids, and variable pH. A marine line may see seawater continuously but be flushed or cleaned with another chemical. In refinery environments, drain and effluent systems can experience a changing mixture rather than one stable fluid. These details should be submitted for compatibility review before the pipe is released for manufacture.
Chemical compatibility is also a joint issue. If adhesive-bonded joints are used, the bonding material and curing process need to suit the service condition. A system should not be judged only by the chemical resistance of its pipe laminate. Gaskets, seals, flange materials, and transition components need to be included in the same review.
Joints and Installation Often Decide Field Performance
Many GRE piping problems are installation-control problems disguised as material problems. Bonded joints require correct surface preparation, adhesive mixing, insertion depth, alignment, cure conditions, and traceability. Lamination work requires similar discipline. If dust, moisture, poor fit-up, or rushed curing enters the process, the line may not achieve the expected joint performance even when the pipe itself is manufactured correctly.
This is why an evaluator should ask early how the supplier supports field assembly. The answer should cover documented joining procedures, installer training or supervision, inspection hold points, repair methods, hydrotest planning, and the management of joints made in hot, cold, humid, or confined work areas. On remote oilfield projects, logistics can influence quality: adhesives and consumables must be stored properly, and the installation team must have the correct tools rather than improvising with general-purpose equipment.
Flanged connections require their own attention. Over-tightening can damage composite flange faces, while uneven bolt loading can create local stress concentrations and leaks. Torque values, bolt sequence, gasket selection, and flange alignment should come from the system supplier’s instructions and the project specification, not from habits developed for steel piping.
Supports, Routing, and Mechanical Loads Need a Composite Mindset
GRE is valued for corrosion resistance and lower weight, but lower weight does not mean supports can be treated casually. Support spacing, saddle geometry, clamp design, guide locations, and protection against point loading all matter. A narrow steel clamp intended for metal pipe can introduce concentrated stress into a composite pipe wall. Abrasion at supports, vibration near pumps, and repeated movement against a structure can progressively damage the outer surface.
Buried pipe needs a separate soil and installation review. Trench preparation, bedding, sidefill, compaction, groundwater conditions, traffic loads, and connection to rigid structures can affect long-term deflection and stress. A buried GRE line should not be specified as if it were simply a lighter steel pipe. The manufacturer’s installation guidance and the project civil design need to be aligned.
The same principle applies offshore and marine applications. Ship motion, equipment vibration, cramped routing, fire-zone boundaries, and interfaces with metal systems can change the design priorities. Corrosion resistance remains attractive, but mechanical restraint and certification requirements must be assessed project by project.
Standards and Documentation: Ask What the Rating Is Based On
An acceptable specification should identify the governing project code, customer standard, and any applicable national, marine, or owner requirements. Depending on the location and service, GRE piping may be evaluated against standards such as ISO 14692 for petroleum and natural gas industries, or other project-mandated composite piping requirements. The relevant standard must be confirmed for the actual installation; it should not be assumed from a previous project.
Beyond a standard reference, evaluators should request the documents that make the design review possible: dimensional data, pressure-temperature qualification information, resin and reinforcement details at the level appropriate for the project, joint procedures, fitting data, test procedures, quality records, and installation instructions. For a critical line, clarity on design life, safety factors, permissible operating conditions, and test pressure is more useful than broad statements about product durability.
Manufacturing capacity can also be relevant when a project includes a large volume of pipe and fittings or a compressed schedule. Shandong Ocean Pipe Technology Co., Ltd., established in 2012 in Wucheng Industrial Park, Dezhou, operates 16 winding production lines, 174 pipe-fitting winding machines and winding micro-control systems, along with five static water-pressure testing machines. Its stated annual GRE pipe production and testing capacity is 25,000 tons. Those figures do not replace project-specific qualification, but they are useful context when assessing whether a supplier can coordinate pipe, fittings, testing, and delivery at scale.
A Practical Evaluation Sequence for Refinery and Oil & Gas Projects
For a refinery application, a disciplined review is usually faster than resolving mismatches after purchase order release. A solution such as GRE Pipe for Refinery should be assessed against the line’s actual fluid, temperature excursions, design pressure, and interface conditions rather than selected solely because GRE has performed well elsewhere in the facility.
A useful sequence is to freeze the process envelope first, including upset cases and cleaning media. Next, establish whether internal pressure, external pressure, thermal cycling, or mechanical loading is likely to govern. Then review material compatibility and the proposed resin system. After that, examine joints, fittings, steel transitions, supports, flexibility, and installation access as one system. Only then should the commercial comparison be finalized.
This approach avoids a common procurement mistake: comparing unit prices for pipe lengths while leaving fitting complexity, field jointing, test support, and installation responsibility unresolved. A lower initial pipe price can lose relevance if the project later needs unplanned engineering changes, special transitions, or rework at difficult site locations.
The Better Selection Is the One With Fewer Hidden Assumptions
Glassfiber Reinforced Epoxy Pipe can be a strong choice for corrosive pressure service when its use is matched carefully to the operating envelope. Its advantages are most credible when the evaluator verifies pressure-temperature limits, chemistry, vacuum conditions, surge exposure, joint integrity, supports, and installation control together.
Before approving a GRE system, ask for the data behind the rating, not just the rating itself. Confirm what happens during hydrotest, shutdown, chemical cleaning, and thermal movement—not only during normal flow. That is usually where a technically sound selection separates itself from a pipe specification that merely looks complete on paper.
Please give us a message
产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍
Please give us a message
产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍
Please give us a message
产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍
Please give us a message
产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍