Acceptance Tests for Glassfiber Reinforced Epoxy Pipe in Oil Projects
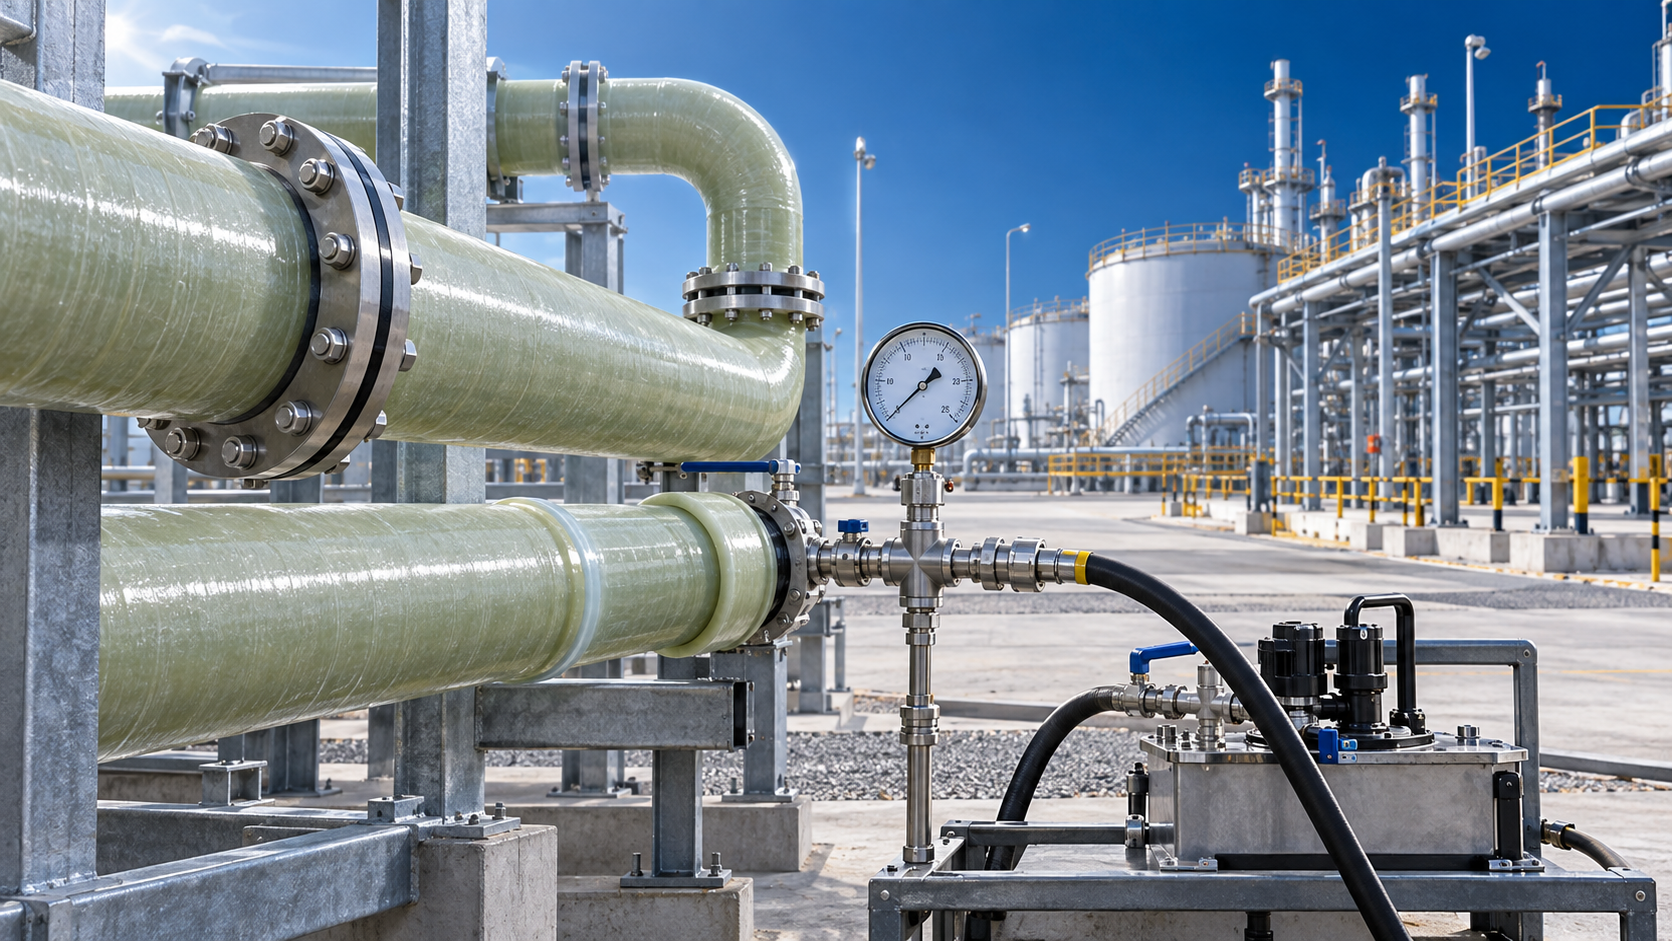
Acceptance testing for Glassfiber Reinforced Epoxy Pipe in oil projects is not a single hydrostatic test performed before shipment. It is a controlled verification that the pipe system delivered to site matches the approved design basis, manufacturing qualification, material traceability, pressure class, dimensional requirements, and installation conditions defined for the project.
The central control point is simple: a pipe may pass a pressure test and still be unacceptable if its resin system, laminate construction, joint configuration, fittings, documentation, or field installation do not match the service duty. In oil and gas applications, this distinction matters because the consequence of leakage can extend beyond production loss to fire, environmental release, personnel exposure, and difficult repair work in remote or hazardous areas.
Acceptance begins with the governing specification
Before inspecting a delivered Glassfiber Reinforced Epoxy Pipe, the project team should establish which document controls acceptance. For oil and gas GRP/GRE piping, ISO 14692 is widely used as a technical reference because it addresses glass-reinforced plastics piping for petroleum and natural gas industries, including design, manufacture, installation, and operation. However, ISO 14692 does not replace the project specification. Purchase orders, client engineering standards, approved data sheets, piping classes, and local regulatory requirements may impose additional conditions.
This is especially important where the same nominal pipe diameter is used in different duties. A line carrying produced water, seawater injection water, firewater, oily drains, chemical dosing fluid, or a hydrocarbon-containing process stream may require different resin systems, pressure ratings, temperature limits, joint designs, and inspection levels. Acceptance should therefore be tied to the line list and approved piping class rather than to a generic statement that the pipe is “GRE.”
A robust inspection release package normally identifies the manufacturer, purchase order, line item, pipe size, pressure class, resin type, reinforcement system, joint type, design temperature range, and applicable standard. It should also distinguish between pipe, fittings, flanges, adhesive-bonded joints, laminated joints, and any special fabricated pieces. Treating these as one uniform product category creates gaps in quality control.
Material traceability is a safety control, not paperwork
GRE performance depends on the interaction between glass reinforcement, epoxy resin, curing system, laminate architecture, liner construction, and manufacturing process. A visual inspection cannot confirm these variables. The acceptance record therefore needs sufficient traceability to connect finished pipe and fittings with the approved raw materials and production records.
Traceability should allow the inspector to establish, at minimum:
- the resin and curing system used for the production batch;
- the glass reinforcement type and product identification;
- the pipe or fitting serial number, lot number, or other permanent identification;
- the production date and relevant curing record;
- the approved manufacturing procedure or qualified laminate design;
- the test reports assigned to the supplied lot.
Where chemical resistance is critical, the resin designation must be checked against the actual fluid composition and operating temperature, not only against a broad description such as “corrosion resistant.” Produced fluids can contain hydrocarbons, dissolved gases, chlorides, scale inhibitors, biocides, acids, or cleaning chemicals. A resin system suitable for one water service is not automatically suitable for another fluid or temperature condition.
Documentation should also show that fittings are compatible with the pipe system. A fitting made with a different laminate thickness, winding angle, reinforcement sequence, or resin system can become the weak point even when straight pipe meets its stated pressure class.
Visual and dimensional examination should focus on service-relevant defects
Visual inspection is often the first physical acceptance activity, but it should not become a superficial search for cosmetic imperfections. The concern is whether observable conditions indicate damage, incomplete cure, laminate discontinuity, contamination, or a defect likely to compromise pressure containment or joint integrity.
Relevant conditions include exposed or broken glass fibres, dry areas, delamination, blisters, cracks, resin-rich or resin-starved zones, embedded foreign material, damaged liners, deep scratches, impact damage, and distortion at pipe ends. Surface marks from handling may be acceptable if they do not penetrate the protective resin-rich layer or affect the structural laminate. The acceptance threshold should be defined by the manufacturer’s approved repair criteria and project requirements, rather than by subjective judgement at the receiving point.
Dimensions must be checked against the approved drawings and applicable tolerances. This includes outside diameter, wall thickness where measurable, overall length, pipe-end preparation, flange dimensions, bolt-hole alignment, socket depth, spigot dimensions, and fitting geometry. For adhesive-bonded joints, dimensional accuracy is directly related to bond-line performance. A pipe that is within general diameter tolerance may still be unsuitable for a specific coupler or socket if the joint dimensions fall outside the qualified bonding range.
Ovality deserves attention after transportation and storage. Composite pipe can be damaged by incorrect support spacing, point loading, stacking beyond the manufacturer’s limit, or lifting practices that concentrate load at one location. A pipe that has been visibly flattened or distorted should not be accepted solely because no crack is evident.
Pressure testing: what it proves and what it does not
Hydrostatic testing is a primary acceptance tool because it can reveal leakage, structural weakness, poor joint assembly, and damage that is not visible externally. It is also commonly preferred to pneumatic testing because water stores far less releasable energy than compressed gas. That does not mean hydrostatic testing is risk-free: test boundaries, restraints, temporary closures, venting, pressurization rate, exclusion zones, and pressure gauges must all be controlled.
The test pressure, hold period, allowable pressure variation, stabilization period, and acceptance criteria must come from the approved project procedure. They should not be selected by applying a generic multiplier to operating pressure. Composite piping may have system-specific test limitations based on design pressure, temperature, joint type, support arrangement, and manufacturer instructions.
During testing, inspectors should verify that the system is completely filled and adequately vented. Trapped air can make pressure behavior difficult to interpret and can create a hazardous energy release if a component fails. Gauges should have suitable range and valid calibration, and their location should allow the test pressure at the relevant test section to be determined accurately.
Acceptance is not limited to “no visible leak.” The inspector should examine joints, flange faces, threaded or bolted connections where applicable, temporary test closures, fittings, branch connections, and repaired areas. Any weeping, sweating, pressure loss outside permitted limits, audible cracking, visible laminate movement, or joint displacement requires engineering review. Repressurizing repeatedly to see whether a leak disappears is not a corrective action.
A successful hydrotest demonstrates the integrity of the tested assembly under the defined conditions. It does not independently prove long-term resistance to cyclic pressure, elevated temperature, chemical exposure, ultraviolet degradation, external mechanical damage, or installation loads. Those characteristics rely on the qualified design and the controlled manufacturing process.
Factory qualification tests and project acceptance tests serve different purposes
Confusion often arises when type tests, routine production tests, and site acceptance tests are treated as interchangeable. They are not.
Qualification testing establishes whether a defined pipe system and joint design can achieve the claimed performance when manufactured within specified parameters. Depending on the governing standard and project requirements, this may include long-term hydrostatic performance evaluation, pressure testing, axial or bending-related verification, joint testing, and chemical or temperature-related assessment. These tests support the design basis; they are not normally repeated on every length of pipe supplied to a project.
Routine production testing verifies that actual manufactured items conform to the qualified system and production controls. It may include dimensional checks, visual examination, cure verification where specified, hydrostatic testing of selected items or batches, and review of manufacturing records.
Site acceptance testing verifies the integrity of the installed system. It is sensitive to field variables that factory testing cannot reproduce, including cut pipe ends, bonding quality, support spacing, field-applied laminates, alignment, flange assembly, and transport damage. A factory test certificate cannot replace a properly controlled system test after installation.
Joint acceptance requires more discipline than straight-pipe acceptance
Many GRE pipe failures originate at joints rather than in the barrel of the pipe. Adhesive-bonded socket joints and laminated joints are highly dependent on surface preparation, mixing ratio, adhesive storage, working time, ambient temperature, humidity where relevant, insertion depth, alignment, and cure time. These variables need documented control.
For bonded joints, acceptance records should identify the trained or qualified installer, joint number, adhesive batch, preparation method, ambient conditions if required by the procedure, assembly time, and cure release status. The purpose is not to create excessive paperwork; it is to ensure that a failed joint can be investigated and that unverified joints do not enter service.
Field crews should not compensate for poor fit-up by adding excessive adhesive, forcing misaligned pipe into a socket, or shortening the prescribed cure period to recover schedule. Such actions may conceal a nonconforming joint until the system is pressurized or exposed to thermal movement.
Bolted flange connections also need specific checks. Correct flange face condition, gasket compatibility, bolt material, tightening sequence, torque control, and alignment are all relevant. Composite flanges can be damaged by over-tightening, while insufficient tightening may produce leakage. Steel-side flange rigidity and piping support arrangement can also affect the composite connection.
Installation conditions can invalidate an otherwise compliant supply
A delivered pipe system should not be accepted as ready for service until installation conditions have been reviewed. GRE pipe has different stiffness, thermal expansion behavior, support requirements, and point-load sensitivity from steel pipe. It should not be installed using support assumptions copied from a steel piping specification without confirmation.
Acceptance checks should cover support type and spacing, restraint locations, allowance for thermal movement, protection at clamps, minimum bend radius where relevant, avoidance of unsupported heavy valves or instruments, and separation from sharp steel edges. Buried pipe requires additional attention to trench condition, bedding, sidefill, compaction, depth of cover, and protection against rock contact or settlement.
Interfaces with metallic pipe require careful design review. Differential thermal movement, galvanic considerations, grounding requirements, flange loads, and transition-piece details should be addressed before commissioning. A pressure-tight test result may not reveal an interface that will become overstressed during temperature cycling or equipment vibration.
Records should support release, investigation, and future maintenance
The final acceptance dossier should make it possible to answer three questions years later: what was installed, under which approved basis, and what evidence showed it was acceptable at handover?
A practical dossier commonly includes approved drawings and line identification, material certificates, production and inspection records, dimensional reports, nonconformance and repair records, joint logs, installer qualifications, hydrotest procedures and signed results, gauge calibration evidence, and as-built information. The format may vary by project, but traceability should survive handover to operations.
The same disciplined approach applies to related composite pressure-retaining equipment. For example, an FRP/GRE Membrane Housing should not be accepted using pipe criteria alone; its pressure boundary, end closures, loading arrangement, and manufacturer-defined test requirements must be evaluated as a distinct equipment item.
Reliable acceptance of Glassfiber Reinforced Epoxy Pipe is therefore not achieved by relying on a certificate, a visual check, or a single hydrotest. It is achieved when design conformity, manufacturing evidence, physical condition, joint quality, installation readiness, and test documentation all point to the same conclusion: the installed system is suitable for the specified oil-project duty and has been released on evidence rather than assumption.
Please give us a message
产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍
Please give us a message
产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍
Please give us a message
产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍
Please give us a message
产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍产品介绍